

 Tiếng Việt
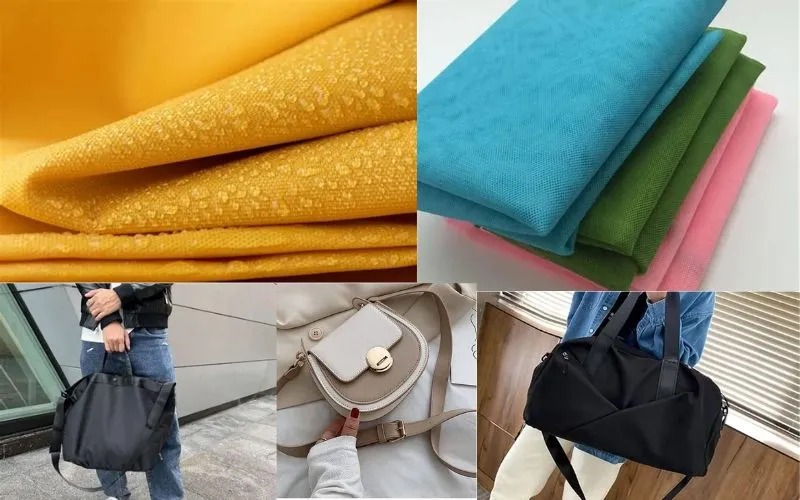
Nylon bag sewing fabric is leading the trend in modern bag production with superior advantages in durability and water resistance. Hop Phat imports a diverse range of high-quality nylon fabrics, from 210D, 420D to 600D nylon, meeting all production needs for fashion bags and medical emergency bags. Below are detailed characteristics of this material type.
I. Basic Concepts About Nylon Bag Sewing Fabric
Nylon fabric is a type of synthetic material created from polyamide polymers. This complex production process creates fabric fibers with high durability and excellent resistance. In the bag manufacturing industry, nylon fabric is favored for its superior properties that few other materials can match.
1. Outstanding Characteristics of Nylon Fabric
High durability is the first strength of nylon fabric. With a tight molecular structure, this fabric type can withstand strong pulling force without tearing. Natural water resistance helps protect belongings inside bags from weather effects.

Lightweight is another advantage that cannot be ignored. Compared to traditional materials like canvas or leather, nylon fabric is significantly lighter while still ensuring sturdiness. This is especially important when producing travel backpacks or sports bags.
2. Classification by Weave Structure
Woven nylon fabric has a tight structure with perpendicularly interwoven fibers. This type is commonly used for products requiring high durability such as office bags or laptop backpacks.
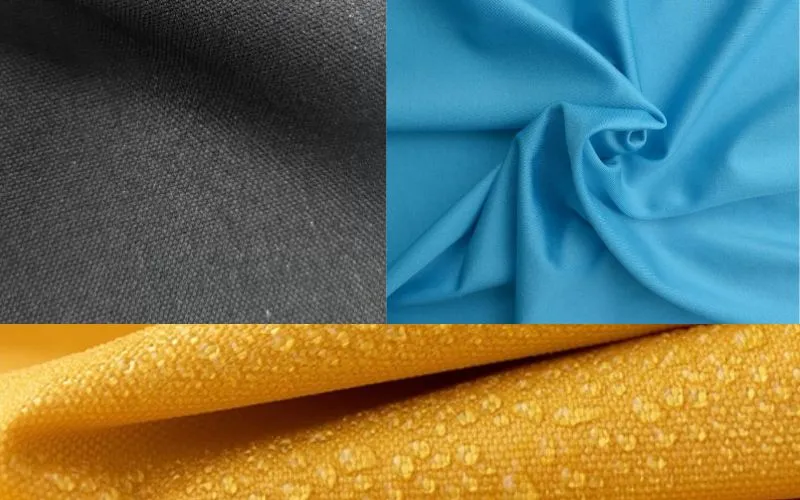
Knitted nylon is softer and more stretchable. However, durability is not as good as woven type, so it’s often used for fashion bags or products not requiring high load-bearing.
Non-woven nylon fabric is the most modern technology, creating material that is both durable and flexible. This special production process brings superior properties to premium bags.
II. Top 7 Most Popular Nylon Fabrics
1. Polyester 600D PU/PVC – King of Materials
Polyester 600D is the golden standard in the bag manufacturing industry. The number 600D (Denier) indicates fiber density, meaning 600 grams for 9000 meters of fiber. The higher the D number, the thicker and more durable the fabric.

PU coating (Polyurethane) provides excellent waterproofing. Meanwhile, the PVC layer (Polyvinyl Chloride) enhances durability and wear resistance. This combination creates perfect material for waterproof bags.
Standard thickness of this fabric type is 0.45mm with a weight of 320g/m². Waterproof capability reaches IPX4 level, can resist drizzle and high humidity. Tensile strength up to 180N ensures bags won’t tear even when carrying heavy items.
2. Nylon Ripstop – Advanced Anti-Tear Technology
Ripstop technology is a breakthrough in nylon fabric production. The reinforced fiber system is woven in a special grid pattern, preventing tears from spreading. When a small point is punctured, the tear will stop right at the nearest reinforcing fiber.

Main applications of this fabric are travel bags, mountain climbing backpacks, and products requiring extremely high durability. Although costs are higher than regular nylon fabric, the lifespan extends 3-4 times longer.
3. Polyester 420D – Smart Economic Choice
With optimal price/quality ratio, Polyester 420D becomes the top choice for large-scale production. Although thinner than 600D type, it still ensures necessary durability for regular bags.
Lower costs about 30% compared to 600D but still has good water resistance. This helps manufacturers optimize costs without affecting final product quality.
4. Nylon 70D – Super Light for Foldable Bags
Nylon 70D is specially designed for products requiring super lightweight. With thickness of only 0.1mm, this fabric type is perfect for foldable bags and portable shopping bags.

Although thin, durability is still surprising thanks to modern weaving technology. Foldability helps save storage and transportation space.
5. Polyester 1680D – Super Durable for Heavy-Duty Bags
Polyester 1680D is the choice for applications requiring extremely high durability. With fiber density double that of 600D type, this material can withstand large loads without deformation.
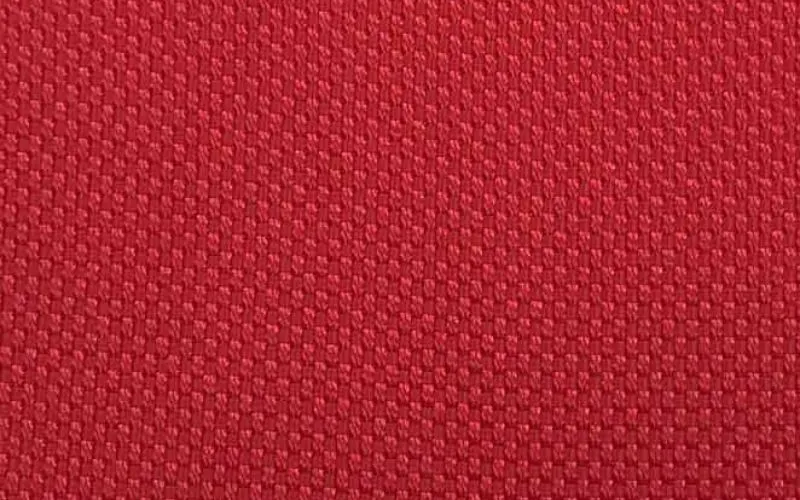
Main applications include luggage, tool bags, and military backpacks. Higher costs but in return is a lifespan that can reach 10-15 years.
6. Oxford 600D Fabric – Versatile and Popular
Oxford fabric has a special weave structure creating a unique texture surface. The 600D type combines high aesthetics with good durability, suitable for many different bag types.

Outstanding advantage is the ability to dye colors evenly and maintain color long-term. This is important for fashion products requiring eye-catching colors.
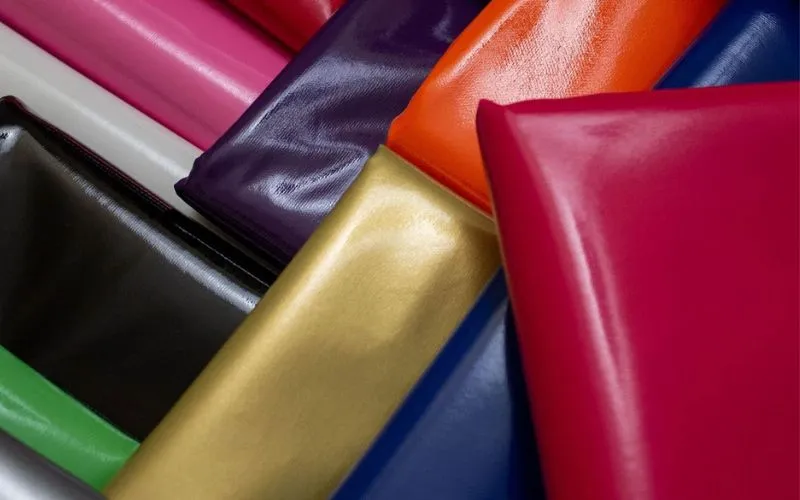
7. Simili PVC/PU Fabric – Premium Faux Leather
Simili fabric provides elegant appearance like genuine leather but at lower costs. The PVC or PU layer pressed onto the surface creates a leather-like texture naturally.
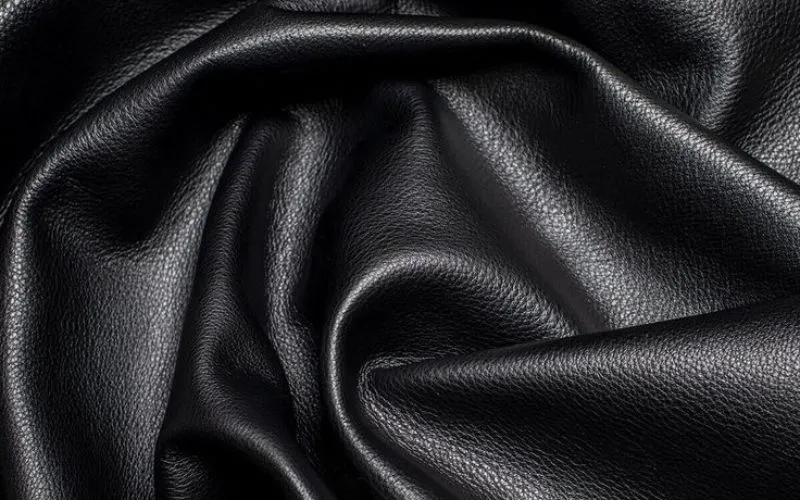
Water resistance of Simili fabric is almost absolute, suitable for premium bags and long wallets. The surface is easy to clean with just a damp cloth.
III. Guide to Choosing Suitable Fabric for Needs
1. Define Specific Usage Purpose
Fashion bags need to emphasize aesthetics over durability. Polyester 420D fabric with many colors and good printing capability will be a suitable choice. Smooth surface and moderate thickness help create elegant lines.

Student backpacks require high durability as they must bear the weight of books daily. Polyester 600D or Nylon Ripstop will ensure long-lasting products without tearing or deformation.
Travel bags need absolute waterproofing and extremely high durability. Polyester 1680D with thick PVC coating is the optimal choice for long trips.
2. Consider Reasonable Budget
Budget segment (25,000-40,000 VND/meter) includes Polyester 420D and basic Oxford 600D. These fabric types are suitable for large-scale production with medium quality requirements.
Mid-range segment (45,000-70,000 VND/meter) has high-quality Polyester 600D PU/PVC and Nylon 70D. This is a good balance between quality and price.
Premium segment (80,000-150,000 VND/meter) includes Nylon Ripstop, Polyester 1680D, and premium Simili PU. These fabric types provide superior quality and high lifespan.
3. Evaluate Durability by Denier (D)
Denier number is the most important index when evaluating fabric durability. 70D suitable for light bags, 420D for regular bags, 600D for load-bearing bags, and 1680D for heavy-duty applications.
However, high Denier is not always best. Need to balance durability, weight, and usage purpose to have appropriate choice.
4. Check PU/PVC Coating Layer
PU coating layer is softer and more environmentally friendly than PVC. However, PVC has better durability and chemical resistance.
Coating thickness is also important. Thin layer (0.1-0.2mm) for basic waterproofing, thick layer (0.3-0.5mm) for complete waterproofing.
5. Consider Origin and Certification
International quality certifications like OEKO-TEX, REACH, or RoHS ensure fabric is safe for user health. Clear origin helps trace and ensure stable quality.
IV. Future Trends of Nylon Fabric
1. Recycled Nylon Fabric – Green Trend
Recycled nylon fabric from plastic bottles and ocean waste is becoming a strong trend. Modern recycling process can create fabric with quality equivalent to new fabric but more environmentally friendly.
Cost of recycled fabric is currently 15-20% higher than regular fabric, but the declining trend is happening rapidly. Consumers increasingly prefer sustainable products.
2. Nano Coating Technology
Nano technology brings new properties to nylon fabric. Nano coating can create self-cleaning, antibacterial, and anti-UV capabilities without affecting the fabric’s mechanical properties.
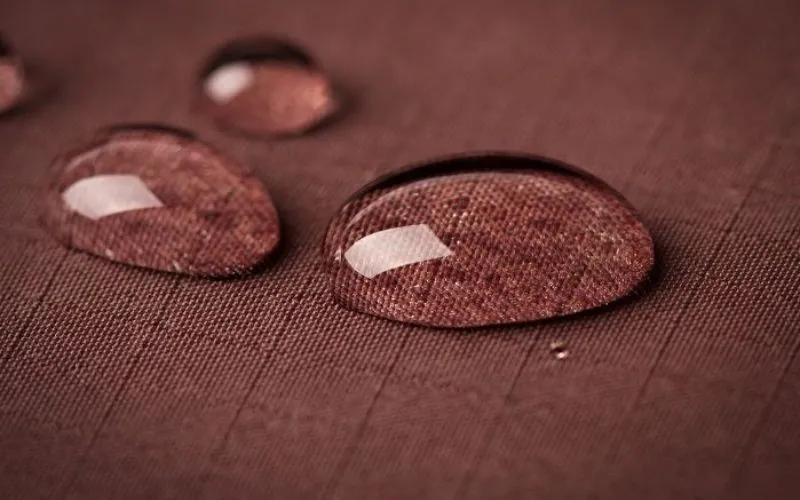
Practical applications have appeared in medical bags and children’s backpacks. Costs are currently high but have potential for wide commercialization in the next 3-5 years.
3. Market Forecast 2025-2027
Nylon fabric market is expected to grow 8-12% annually. Demand for high-quality and environmentally friendly fabric will be the main driver.
Prices are expected to stabilize with slight declining trend thanks to technology improvements and increased production scale. Quality will be standardized higher.
Through the above information, you clearly understand the superior advantages of nylon bag sewing fabric. From water resistance features, easy cleaning to diverse printing capabilities, every factor is perfect. Start your successful bag business journey right now. Order large quantities of bags to receive attractive discounts up to 20% from Hop Phat manufacturing.